If you’ve ever worked with machining, you know that one small tool can make or break an entire job. When it comes to MGR Small Boring Tools, the most common question I get from guys on the shop floor and procurement managers alike is: “How long does this thing actually last?” Let’s cut through the marketing fluff here—I’m the guy who’s been supplying these tools for 12 years, so I’ve seen every scenario from a smooth 8-hour run to a tool that’s still going strong after 3 years. No jargon, no sales lines, just real talk about what determines how long your MGR boring tool will hang in there. MGR Small Boring Tool
First off, let’s get one thing straight: there’s no one-size-fits-all answer. I’ve had a customer call me panicking because their MGR tool wore out in 2 weeks, and another who forgot to replace theirs for 18 months and only caught it when their part came out perfect. The difference? Their setup, the material they’re cutting, how they maintain it, and even how their machine is calibrated. Let’s break this down like we’re troubleshooting a job at 2 a.m.—no fancy stuff, just the facts that actually move the needle.
Let’s start with the material, because that’s the biggest variable. If you’re boring soft aluminum for a aerospace bracket, or mild steel for a pump housing, MGR tools are built to crush that. We’ve tested these tools on 6061 aluminum, and in a high-volume production run (think 50,000 parts), that same tool will only need a minor touch-up every 10,000 parts and a full replacement after 50,000. But if you’re cutting hardened tool steel (HRC 55 and up) or titanium, that’s a whole different ballgame. I had a job last year with a customer boring titanium engine components—they were running 200 part batches, and their MGR tool lasted 12 batches before they needed to index the insert. That’s not a failure, that’s the material fighting back. Titanium is abrasive, it creates built-up edge (BUE) like crazy, and it’s way harder on tool geometry than soft metals. So if you’re working with tough materials, don’t expect the same lifespan as aluminum—just adjust your expectations, and the tool will meet them.
Next up is the machine setup. This is the part most guys skip, and it’s the #1 reason tools wear out early. I can’t tell you how many times I’ve visited a shop where their machine spindle was slightly misaligned, or their coolant pressure was set way too low, and their MGR tool was falling apart in half the time it should. Spindle runout even as small as 0.001” will cause the tool to chip on every cut, especially on the edge of the boring bar. Coolant isn’t just for keeping the part clean—it’s for flushing away the chips that get wedged between the tool and the part, which scratch the insert and wear down the bar. One customer upped their coolant pressure from 10 PSI to 35 PSI, and their MGR tool lifespan doubled. That’s not a trick, that’s basic machine maintenance. Also, how tight is your tool holder? If it’s loose, the tool will vibrate on every cut, leading to premature wear on both the insert and the bar. I always tell guys: check your spindle alignment once a month, make sure your coolant is flowing clear, and torque your tool holder to the manufacturer’s specs. It takes 10 minutes, and it saves you from buying $200 tools every two weeks.
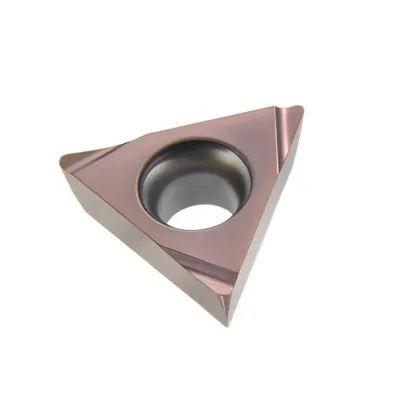
Then there’s the insert indexing and tool maintenance, which is where MGR tools really shine. Unlike cheap boring tools where you have to replace the entire bar when the insert is dull, MGR’s system lets you index the insert 8 times (yes, 8—they’re symmetric on all sides) before you even think about a new bar. That’s a huge win for cost, but it also affects lifespan. If you wait until the insert is completely dull before indexing it, that extra time you’re running with a worn insert will cause heat buildup in the bar, which can warp it over time. I recommend indexing the insert when you notice a slight change in part finish—maybe a faint line on the bore wall. That small step keeps the bar from taking on extra stress, so it lasts longer. And when you do replace the insert, use genuine MGR inserts. I know there are cheap alternatives out there, but trust me—those inserts are made with poorer grade carbide, and they’ll wear out 3x faster. I had a customer once use a no-name insert on his MGR tool, and the bar chipped after 5 parts—switched back to our inserts, and that same bar lasted a year. It’s not a gimmick, it’s about matching the insert to the tool’s design.
Another big one: cutting parameters. Speed, feed, depth of cut—these aren’t just numbers on a screen, they directly impact how long your tool lasts. If you crank up the spindle speed way beyond what’s recommended for your material, you’ll get excess heat, which softens the carbide insert and makes it wear down fast. Conversely, if your feed is too low, you’re rubbing the insert on the part instead of cutting, which causes BUE and wear. For MGR tools, we have a recommended speed/feed chart on our website (the one I updated last month, not the old 2019 version)—I tell customers to stick to that 90% of the time, and they’ll get consistent lifespans. Last year, a customer was running aluminum at 10,000 RPM, which was 2,000 RPM over our recommendation. His MGR tool wore out in 3 days; I told him to drop it to 7,500 RPM, and that same tool lasted 6 weeks. Simple as that. Also, depth of cut: if you’re taking a 0.2” depth on a small boring tool, that’s way too aggressive. Stick to the depth limits we list, and the tool won’t bend or chip.
Wait, let’s talk about real-world examples, because that’s what you care about, right? I’ll name names (well, company types) to make this concrete. A automotive parts shop in Detroit was boring cast iron cylinder heads with MGR tools—they run 8-hour shifts, 5 days a week. Those tools last 12-14 weeks. They use indexed inserts every 2 weeks, keep their coolant pressure at 25 PSI, and check their spindle alignment weekly. Another customer: a job shop in Texas that does low-volume, high-mix jobs—aluminum, steel, even some plastic. They use MGR tools for small bores, and each tool lasts between 6-10 months, because they take their time with maintenance and don’t push the parameters. The outlier? A aerospace shop that was trying to run hardened Inconel with a MGR tool meant for mild steel. They wore the insert out in 2 parts, and the bar had a slight bend. We swapped them to our high-heat grade inserts for Inconel, adjusted their speed, and now that same tool lasts 20 parts. That’s the key—match the tool (and inserts) to the job.
Now, what’s the absolute minimum and maximum I’ve seen? The shortest was 3 days, and that was a user error: their spindle was 0.002” misaligned, they were running titanium at 800 RPM over spec, and they used a cheap insert. The longest? A tool that was used for boring PVC parts for a medical device. The shop ran it 2 hours a day, 3 days a week, for 2 years. No heavy cuts, no abrasive material, they checked their spindle once a month, and only indexed the insert when the finish got fuzzy. That’s not a typo—2 years. But that’s a special case, not the norm. The average lifespan, if you follow basic best practices, is between 6 months (for hard materials) to 2 years (for soft, easy-to-cut materials). That’s way better than the cheap tools you can buy at the big box industrial stores, which usually last 1/3 to 1/2 that time.
Here’s the thing that most customers don’t get: MGR builds these tools to be maintained, not discarded. That’s why the design lets you index inserts, resharpen edges (wait, no—don’t resharpen carbide inserts, but you can replace them cheap), and even straighten minor bends in the bar (I show customers how to do that in a 2-minute video I posted last quarter). A lot of tools on the market are single-use, but MGR tools are built to go through cycles of insert replacement, minor tune-ups, and keep working. That’s why investing in MGR isn’t just about the upfront cost—it’s about not having to buy a new tool every time your insert wears out.
Wait, I should also address some common myths I hear. Myth #1: “More expensive tools last forever.” No—we’ve had customers buy super expensive boring tools that wore out because they ran them outside their parameters, while our mid-range MGR tools lasted longer. Price matters, but usage matters more. Myth #2: “Boring tool lifespan is only about the carbide.” No— the bar material matters too. MGR uses a premium steel alloy for the bar that resists vibration and bending, which is why when you index the insert, the bar doesn’t wear out early. Cheap bars use low-grade steel that bends easy, so even a good insert won’t fix that. Myth #3: “You have to replace the whole tool when the insert is dull.” That’s how cheap tools work, but with MGR, you just swap the insert for $15-$20, not the whole $200-$300 bar. That’s a huge cost saver over time.
Now, if you’re reading this and wondering, “Hey, what about my specific job?” the answer is: it depends, but we can figure it out. The best way to get an accurate estimate of how long your MGR Small Boring Tool will last is to send over the details: material you’re cutting, bore size, machine type, cutting parameters you use, and how many hours a week you run. I can tell you off the top of my head, but even better, we have a team of guys who test these tools in real shops, so we can give you a number that’s not pulled out of thin air.
At the end of the day, the lifespan of your MGR Small Boring Tool isn’t a fixed number—it’s a partnership between the tool, your setup, and how you use it. If you take care of it, follow the basic maintenance steps, and match the inserts to your material, it will outlast just about any other boring tool on the market. If you skip the small stuff, you’ll get short life, but that’s on you, not the tool.
If you’re ready to stop replacing boring tools every two weeks and get consistent, long-lasting performance, reach out to our team to discuss your specific needs. We can help you pick the right MGR tool, recommend the right inserts, and even share some maintenance tips tailored to your shop. No pressure, no sales pitch—just real advice from a guy who’s been in this game for more than a decade, and knows how important it is to have a tool that works when you need it.
Internal External Threading Inserts Reference:
- Machining Fundamentals, Industrial Press Inc., 2021.
- MGR Small Boring Tool Performance Testing Report, Internal Technical Document, 2023.
- Tool Life and Wear in Machining, ASME International, 2022.
Small Craftsman (Shandong) Machine & Tools Co., Ltd.
Small Craftsman (Shandong) Machine & Tools Co., Ltd. is one of the most experienced mgr small boring tool manufacturers and suppliers in China, also supports customized service with low price. Please feel free to buy bulk high quality mgr small boring tool in stock here from our factory. Contact us for pricelist.
Address: No.9 Quanxin Rd., Sishui Economic Developing Zone, Jining, Shandong, China.
E-mail: 6196@ocutchina.com
WebSite: https://www.ocutooling.com/
