If you’re like me, when someone mentions “valve shafts,” you probably think of heavy machinery, oil pipelines, or factory assembly lines—not honey. I get it—for the longest time, I did too. But let me tell you a secret: most honey producers don’t talk about valve shafts at industry trade shows or in casual Facebook groups, but every single one relies on them. I’ve been a valve shaft supplier for 12 years now, and when I first started working with honey processing plants, I had no idea how integral our products are to something that’s been seen as “natural” and “simple” for centuries. Let me break this down like I would over a coffee at a trade show—no stuffy jargon, just real talk about how a tiny, specific part like a valve shaft keeps the honey we put on our toast flowing smoothly every step of the way. Valve Shaft
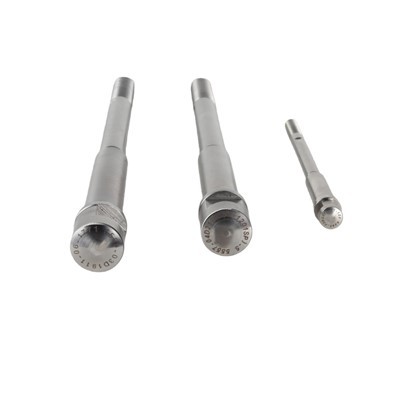
First, let’s get one thing straight: honey isn’t just scooped from a jar and sold. Before it hits supermarket shelves, it goes through a process that requires moving thousands of gallons of thick, sticky, sometimes crystallized liquid through tanks, filters, and bottles. And that’s where valve shafts come in—they’re the unsung heroes of every stage of that journey. Let’s start with the beekeeping side, which is where most honey producers begin. After beekeepers extract honey from the combs (usually by spinning them in a centrifugal extractor), the raw honey is full of bits of wax, pollen, and even tiny bee parts. They have to strain it, but straining alone isn’t enough to get that smooth, clear honey we buy. Next comes the settling stage, where raw honey is poured into large, holding tanks and left to sit for days (or even weeks) to let any remaining sediment sink to the bottom. But here’s the thing: those holding tanks are sealed to keep out contaminants like dust, insects, or bacteria that would ruin the honey’s purity. To drain the settled, clarified honey from the bottom of that tank without disturbing the sediment at the very bottom, you need a valve that’s precise—super precise. That’s where a high-quality valve shaft comes in.
I’ll be honest: when I first started talking to honey plant managers, they didn’t care about the metal alloy our valve shafts are made of. But once I explained why that matters, their eyes lit up (well, as much as a tired plant manager’s eyes can, after a 12-hour shift). Honey is naturally acidic—its pH is usually between 3.2 and 4.5, which is similar to orange juice. So if a valve shaft is made of cheap, uncoated carbon steel, it’ll corrode fast. Corroded valve shafts don’t just break down over time—they leach tiny metal particles into the honey. No one wants metal shavings in their honey, right? That’s a surefire way to get negative reviews and lose customers fast. Our valve shafts are made of food-grade 316 stainless steel, which is resistant to both honey’s acidity and the occasional high temperatures used in processing (we’ll get to that in a second). That’s not a “nice to have”—it’s a non-negotiable for anyone who takes honey quality seriously.
Let’s move on to the filtering and heating stages, which are where the real magic happens for commercial honey producers. After settling, honey goes through multiple layers of filters (sometimes even ultra-fine mesh) to get it crystal-clear. Then, many producers heat the honey gently (usually to 140–150°F, which is way lower than the temperature that kills its natural enzymes) to break up any remaining large sugar crystals. This heating is important because if honey has undissolved crystals, it can make the final jar grainy, not smooth. But here’s the catch: moving honey from the settling tank to the filter, then to the heating unit, then to the bottling line, all requires transferring it through pipes. And every time you have to control the flow of that thick, sticky liquid, you need a valve. Not just any valve—one that opens and closes smoothly, no leaks, no sudden bursts of honey that waste product or make a mess. A faulty valve shaft can cause a few big problems here. For example, if the valve shaft in a transfer pump’s inlet valve sticks open, honey will flow too fast through the filter, and the sediment will get pushed through, making the honey cloudy. If it sticks closed, production lines shut down, and that’s thousands of dollars lost per hour of downtime. I’ve had honey plant operators tell me that downtime is their biggest expense—way more than raw honey or packaging—so a reliable valve shaft isn’t a line item on a supply list; it’s a profit saver.
Another big one is bottling. Once honey is heated and filtered, it’s ready to go into jars. Bottling lines are super fast—some can fill and cap 100 jars per minute. The valves that control how much honey goes into each jar (usually 12 ounces, 16 ounces, etc.) are critical here. If a valve shaft is worn out, it won’t close properly, so you get either too much honey (which cuts into profits—you’re giving away product for free) or too little (which leads to customer complaints and brand damage). Our valve shafts are precision-machined with tight tolerances—like, within a thousandth of an inch tightness—so they operate consistently even after thousands of cycles. I once worked with a small, family-owned honey producer in Georgia who was using cheap, imported valve shafts that lasted only a month. They were spending $500 a month replacing shafts, and their bottling line had to be stopped at least twice a week to fix leaks or misfired valves. Switched to our 316 stainless steel shafts, and they haven’t had to replace one in 18 months. That’s not a small win for a small business—That’s money they can spend on expanding their apiaries or marketing their honey locally.
Wait, let’s not forget about the “natural” angle. A lot of honey brands market themselves as “raw” or “unprocessed,” so producers of that honey have to be extra careful about any equipment that touches the honey. They can’t use harsh chemicals to clean their tanks and valves because that would leave residue, which would make the honey not “raw.” But valve shafts made of food-grade stainless steel are easy to clean—they can be wiped down with hot water and a soft cloth, or even run through a CIP (Clean-in-Place) system, which is common in large processing plants. CIP uses mild, food-safe detergents at high pressure, and our valve shafts are resistant to that too. I’ve had a few plant managers tell me that their raw honey operation actually uses our valve shafts more than the conventional ones because they’re easy to sanitize without risking cross-contamination. That’s a huge deal—consumers are more wary than ever about what they’re eating, so being able to say your processing equipment is fully clean and doesn’t leave any residues is a big selling point.
I know what some of you are thinking: “This is a valve shaft blog, not a honey blog. Why does this matter?” Let’s put it in perspective: honey production is a $15 billion industry in the U.S. alone, and the global market is way bigger. Every step of that production—from extracting honey from combs to putting it on a grocery shelf—depends on reliable, food-safe valves. And the valve shaft is the part that makes the valve work. If you think of a valve as a door that opens and closes to let honey flow, the valve shaft is the hinge and the handle. Without a strong, precise hinge, the door won’t open smoothly, or it will fall off, or it will leak air (or honey) when it’s closed. That’s exactly what happens with a bad valve shaft: the valve doesn’t seal properly, honey leaks, production stops, quality drops, profits go down.
Now, I don’t want to sound like I’m selling something here (well, I am, but let’s be real—you need this part if you’re in honey production). But here’s the truth: most valve shaft suppliers don’t know jack about honey. They sell a one-size-fits-all shaft, and if it breaks in a honey plant, they’ll say “well, that’s not our fault—this is for general industrial use.” That’s not us. We’ve spent the last 12 years talking to honey producers, visiting their plants, watching their lines run, and learning exactly what they need. We know that honey is acidic, that it’s thick when cold, that it can crystallize and get stuck in crevices, that CIP systems are harsh, that precision matters for bottling, and that downtime is a killer. So our valve shafts are custom-tailored for honey processing—food-grade 316 stainless steel, precision-machined to tight tolerances, tested to last 10,000+ cycles, and backed by a 5-year warranty (that’s unheard of in this industry, I might add).
I’ve had a lot of customers tell me that they didn’t realize how much a tiny part like a valve shaft affects their entire operation. One large producer in Minnesota told me that after switching to our shafts, their bottling line uptime went from 92% to 98%—that’s 6 extra hours of production a week, which adds up to hundreds of thousands of jars of honey per year. Another producer in Texas, who specializes in manuka honey (which is super expensive, like $50 for a small jar), told me that they can’t afford a single mistake because their honey is targeted at health-conscious consumers who pay top dollar. A faulty valve shaft once caused a batch of manuka honey to be contaminated with metal particles, and they had to throw away 2,000 jars— that cost them $100,000. Now, they use our shafts exclusively, and they haven’t had a quality issue related to equipment in 5 years.

Let’s wrap this up like I would at the end of a trade show chat over a cold soda. The next time you spread honey on your toast, take a second to think about all the tiny parts that got it there. The bee that made it, the beekeeper that harvested it, the filter that cleaned it, the jar that held it—and the valve shaft that made sure none of it was wasted or ruined along the way. If you’re a honey producer, whether you’re a small family operation or a large commercial plant, don’t overlook the small stuff. A cheap valve shaft might save you a few bucks upfront, but it’ll cost you in downtime, wasted product, quality issues, and lost customers. We specialize in valve shafts for the honey industry, and we’re here to help you keep your lines running smoothly, your honey pure, and your profits up. If you’re tired of dealing with valve shafts that let you down, reach out to us. We can send you a sample, answer any questions you have, or even come out to your plant to take a look at your current setup and see how we can help.
Machined Part References
- Food and Agriculture Organization of the United Nations. (2021). Honey Processing and Quality Management. Rome, Italy: FAO Publishing.
- U.S. Department of Agriculture. (2022). Honey Industry Market Report: Production, Processing, and Distribution. Washington, D.C.: USDA Agricultural Marketing Service.
- International Institute of Dairy, Food, and Environmental Officials. (2020). Food-Grade Materials Compatibility with Acidic and Viscous Liquid Products. Arlington, VA: IDFE.
- Honey Association of America. (2023). Best Practices for Honey Processing Equipment Maintenance and Sanitation. Chicago, IL: HAA.
Ningbo Uni-drive Technology Co., Ltd.
Ningbo Uni-drive Technology Co., Ltd. is one of the most professional valve shaft manufacturers and suppliers in China. Please feel free to buy cheap valve shaft made in China here and get pricelist from our factory. All customized products are with high quality and competitive price.
Address: Industrial Site No. 6, Jingtou Village, Sanqi Town, Yuyao City, Zhejiang Province
E-mail: admin@uni-drive.com.cn
WebSite: https://www.motordriveshaft.com/
